

A complete-looking report can still stop an aerospace component at receiving inspection. The dimensions may pass, yet the material certificate belongs to another lot, a drawing note has no evidence, or the submitted part was made with a different route from the planned production process.
Aerospace first article inspection, or FAI, is a planned verification and documentation activity used to establish that the production process can produce a part meeting the specified requirements. Passing individual dimensions is only part of that task. A reviewable first article inspection report connects the correct configuration, production article, applicable characteristics and supporting evidence.
This guide addresses the supplier-to-buyer handover for custom components. It is not a replacement for the applicable standard, purchase-order clauses or a customer’s acceptance decision.
Define the first article before production
Start with the contract. Establish the part number, revision, applicable specifications, required FAI scope, submission format and approval timing. Confirm which standard revision and customer supplements apply. Do not wait until packing to discover that the customer requires a particular portal or an approval before shipment.
SAE’s published scope for AS9102C explains that its FAI requirements complement customer and applicable statutory and regulatory requirements. The standard is therefore not a substitute for reading the purchase order. Nor does completing a report establish an organization’s certification or the airworthiness of an assembled aircraft.
Identify the manufacturing configuration represented by the first article: material source, relevant tooling, program, production route, special processes and inspection approach. Record the actual article or lot so evidence cannot become detached from the hardware. A development sample made through a different route must not be presented as production evidence without an appropriate basis.
The parent aerospace quality control and inspection topic covers the broader verification system. This article concentrates on assembling a coherent first-article package and resolving gaps before it reaches the customer.
Separate planning from completion
A plan can be prepared before the part exists. Results cannot. Define how each applicable characteristic will be verified, what records are expected from outside processors and who reviews completeness. Then populate the report with the evidence generated by the actual work, rather than pre-filling expected outcomes.
Three reviews that should agree
A useful internal review separates configuration, product evidence and characteristic accountability. These are practical review questions, not a reproduction of the official forms or permission to replace a customer’s required template.
| Review | What should agree | Typical unresolved mismatch |
|---|---|---|
| Configuration | Order, drawing, model, part identification and applicable revision | The report describes revision B while the purchase order requests revision C |
| Product evidence | Material and process records, traceability and applicable test evidence | A certificate is present but cannot be connected to the delivered parts |
| Characteristic accountability | Design requirements, inspection references, methods and results | A drawing note or repeated feature has no identifiable verification |
Each review should have an owner. The inspector may know the dimensional method but not control the subcontractor’s process certificate. Purchasing may receive a certificate but not recognize that its specification revision differs from the order. A named reviewer must close those interfaces rather than assuming another department has done so.
Keep an explicit status for unresolved items. A blank cell, a note saying pending and a completed acceptance decision are different states. Missing evidence should remain visible until it is supplied or an authorized disposition establishes how the requirement is handled.
Before submission, compare identifiers across the package as well as checking each document separately. A file can be internally correct yet belong to a different part, lot or revision. That is why collecting a folder of certificates is not the same as demonstrating traceability.
Follow one feature through the whole package
Consider a hypothetical mounting bore in a machined aerospace fitting. Its diameter is only one requirement. The released definition may also control its position relative to datums, surface texture, edge condition and final condition after a specified finish. The first article package must address the applicable requirements, not just the easiest measurement.
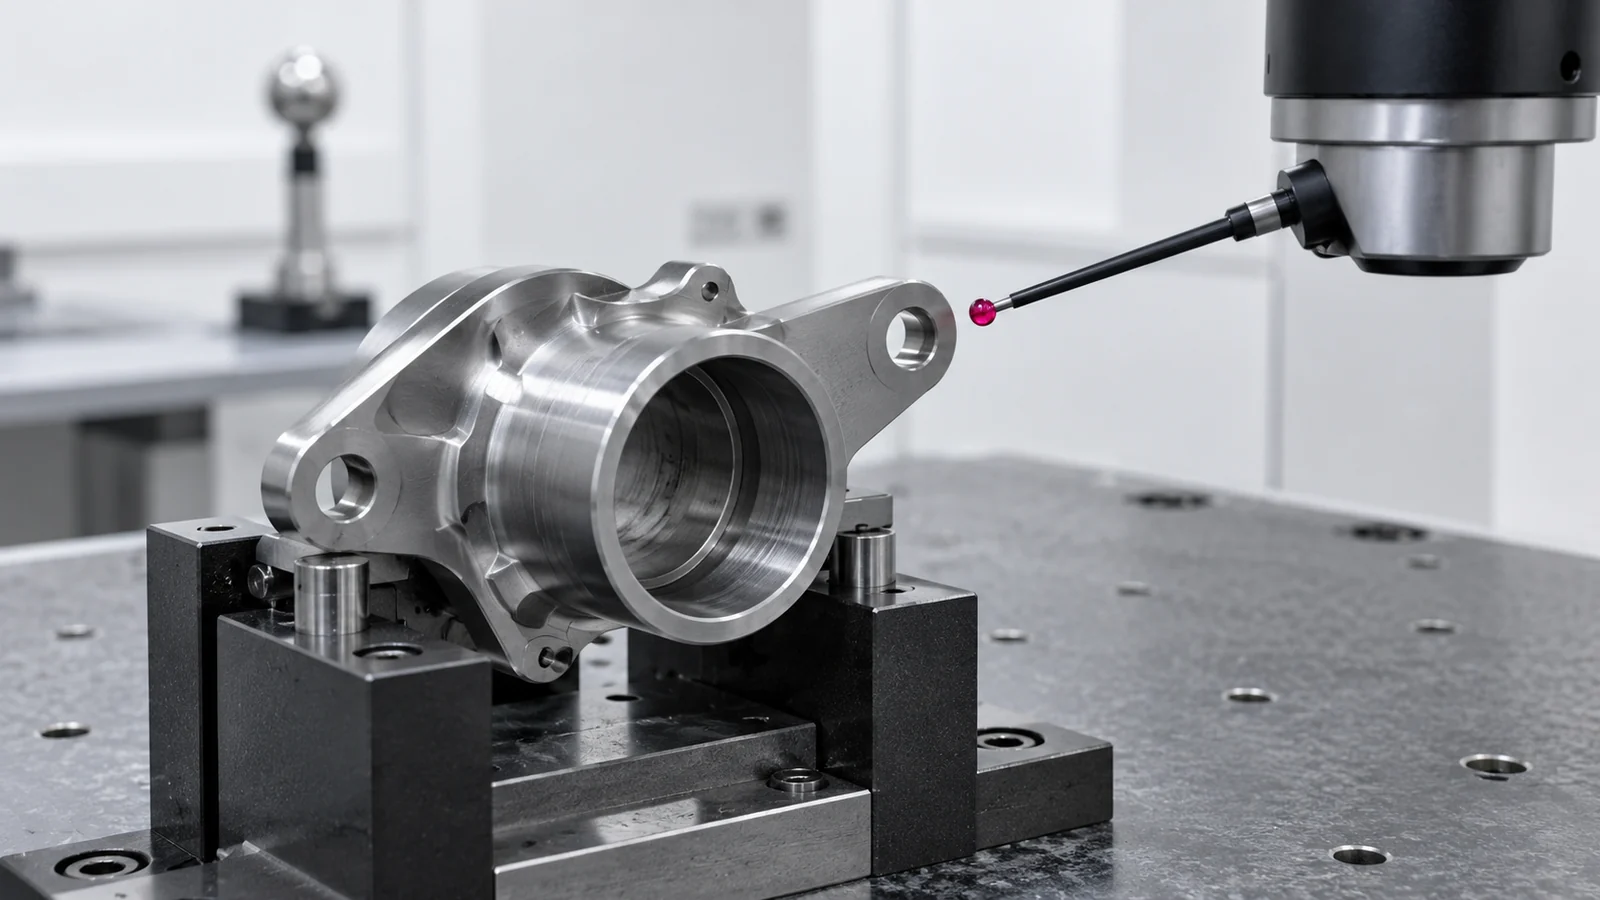
Start at the drawing reference. Locate the corresponding inspection entry and confirm that the units, limits and datum interpretation match. Next, identify the method and actual result. Finally, confirm that the measured component represents the material and manufacturing configuration claimed elsewhere in the package.
If the bore is measured before finishing but the drawing requires a finished condition, the team needs an appropriate verification plan. A statement that coating is thin does not close a dimensional requirement. Equally, a surface finish certificate does not prove the bore’s location unless it provides the relevant evidence through an accepted method.
The same logic applies to non-dimensional characteristics. Trace material requirements to the correct record, and process requirements to the relevant completion evidence. Keep the extent of the claim aligned with what the document establishes. A supplier certificate should not be stretched into proof of unrelated performance.
Use this feature walk-through as a stress test for the package. It does not reduce the requirement to account for other applicable characteristics. Its value is exposing handover failures that a line-by-line form check can miss.
Changed process, changed evidence
An accepted first article is linked to a defined configuration and production process. A later change may affect the validity of that evidence. Review changes to design requirements, manufacturing route, location, tooling, material or inspection as required by the applicable standard and customer contract.
Do not automatically choose either extreme: redoing everything after every administrative edit or assuming that unchanged nominal dimensions mean no further work is needed. Determine which requirements or process assumptions the change could affect, document the assessment and obtain the required approval for full or partial activity.
Example: a revised fixture
Suppose a locating arrangement changes while the product drawing remains unchanged. The change could affect a bore’s location, part restraint or inspection access even though the CAD model is identical. A justified review asks what must be reverified and what prior evidence remains applicable. It does not simply copy the previous report under a new date.
Preserve the relationship between the earlier accepted package and the new evidence. Identify the reason for the update, affected characteristics and production applicability. This lets a later reviewer understand why some evidence was retained while other checks were repeated.
Why technically good parts get held
Delivery acceptance can depend on both conforming hardware and an acceptable submission. A buyer may be unable to release a usable part when its identity or required evidence remains uncertain. This is not solved by replacing missing documentation with assurances about workshop experience.
A concrete example is Northrop Grumman’s quality provision 0722.8. When that clause applies, it specifies reporting through Net-Inspect and additional submission and acceptance conditions. This illustrates customer-specific requirements; it does not mean every aerospace buyer uses the same portal or delivery rule.
- Identity gap: the sample cannot be connected to its work order or supporting records.
- Scope gap: dimensions are recorded but an applicable note remains unverified.
- Timing gap: a required approval was not obtained before dispatch.
- Condition gap: the inspected state differs from the specified delivered condition.
- Authority gap: a deviation was noted but not dispositioned by an authorized party.
Schedule an internal completeness review before the shipping deadline. Ask the intended reviewer to open the actual submission files, follow several cross-references and identify unresolved items. A broken attachment or mismatched revision is easier to correct before the package leaves the supplier.
For a Jucheng Precision quotation involving custom CNC machining, include the required FAI scope with the drawing package. Agree on documentation, outside-process evidence and customer review responsibilities before manufacturing. Specific certification, test and acceptance commitments require project-level confirmation.
Buyer and supplier questions
Is a first-piece dimensional report the same as aerospace FAI?
Not necessarily. A first-piece check may confirm selected setup dimensions. Aerospace FAI can require broader characteristic accountability, product records and customer-defined documentation. Compare the actual scope rather than treating the names as interchangeable.
Does an accepted FAI replace routine production inspection?
No. Production controls and ongoing acceptance requirements still apply. A first article establishes evidence about a defined production configuration; it does not guarantee every later part or eliminate checks required by the control plan and contract.
Can the report be closed with missing test evidence?
Only the applicable requirements and authorized acceptance process can determine its status. Keep missing evidence explicit and follow the agreed disposition. Do not mark the package complete merely because the dimensional rows are filled.

