

ISO 13485 purchasing controls are not finished when a supplier is approved. The buyer must communicate the requirements for a particular product or service, verify what arrives, monitor the provider, and respond when its performance or route changes. For medical-device components, the purchasing process is where the approved design becomes an order that a machine shop, molder, finisher or assembler can actually execute.
This article explains the manufacturing interface rather than reproducing the standard’s clauses. The finished-device organization should determine its applicable regulatory obligations with qualified personnel. A component supplier may be asked to meet defined requirements under a contract; that is different from claiming every supplier has the same legal role or certification.
Supplier Approval Is Only the Entrance Gate

An initial audit or questionnaire tells the buyer something about a supplier at one point in time. It does not confirm that a new order carries the right drawing, resin, finish, inspection method or subcontracting permission. The purchasing system must connect supplier selection with order-level requirements and later monitoring.
Classify providers according to what their output could affect. A stock supplier for a noncritical fixture, a producer of a sealing component and an external cleaning provider may need different evaluation depth. Classification should be justified by the purchased product and its effect on the device, not simply by annual spend or a generic approved-vendor label.
The existing medical device manufacturing standards page explains the broader quality-system context. An audit concentrates on what to observe during supplier evaluation; purchasing controls continue through the order, receipt and performance review.
Build an Order That Cannot Be Misread

Use the released part number and revision, not a file called “final-final.” State the exact material grade or approved specification, finishing state, critical dimensions and the acceptance evidence expected with the shipment. If the buyer requires a particular method or subcontractor approval, make that explicit. Ambiguous language transfers uncertainty to the shop floor.
For example, “316L housing, inspect before shipping” leaves open the stock form, surface condition, critical bore measurement, passivation scope and required records. A good order references controlled documents and explains what version applies. It does not need to reprint a whole drawing, but it must make the authoritative source clear.
Separate product requirements from delivery preferences. A requested ship date is important, but it cannot silently override a required inspection or material source. If the supplier proposes a substitute to meet timing, the buyer needs a controlled technical decision before the new input enters production.
| Purchasing input | Why it matters | Typical ambiguity to remove |
|---|---|---|
| Part and revision | Connects order to approved design | Old drawing in a recurring order |
| Material specification | Defines approved input | Family name used instead of grade |
| Finish and post-process | Defines delivered state | Unspecified provider or masking |
| Inspection basis | Defines acceptance evidence | Unclear datum or sample size |
| Change notice | Protects approved configuration | Supplier decides equivalence alone |
| Records with shipment | Supports release and traceability | Buyer expects data supplier did not price |
Match Verification to the Purchased Risk

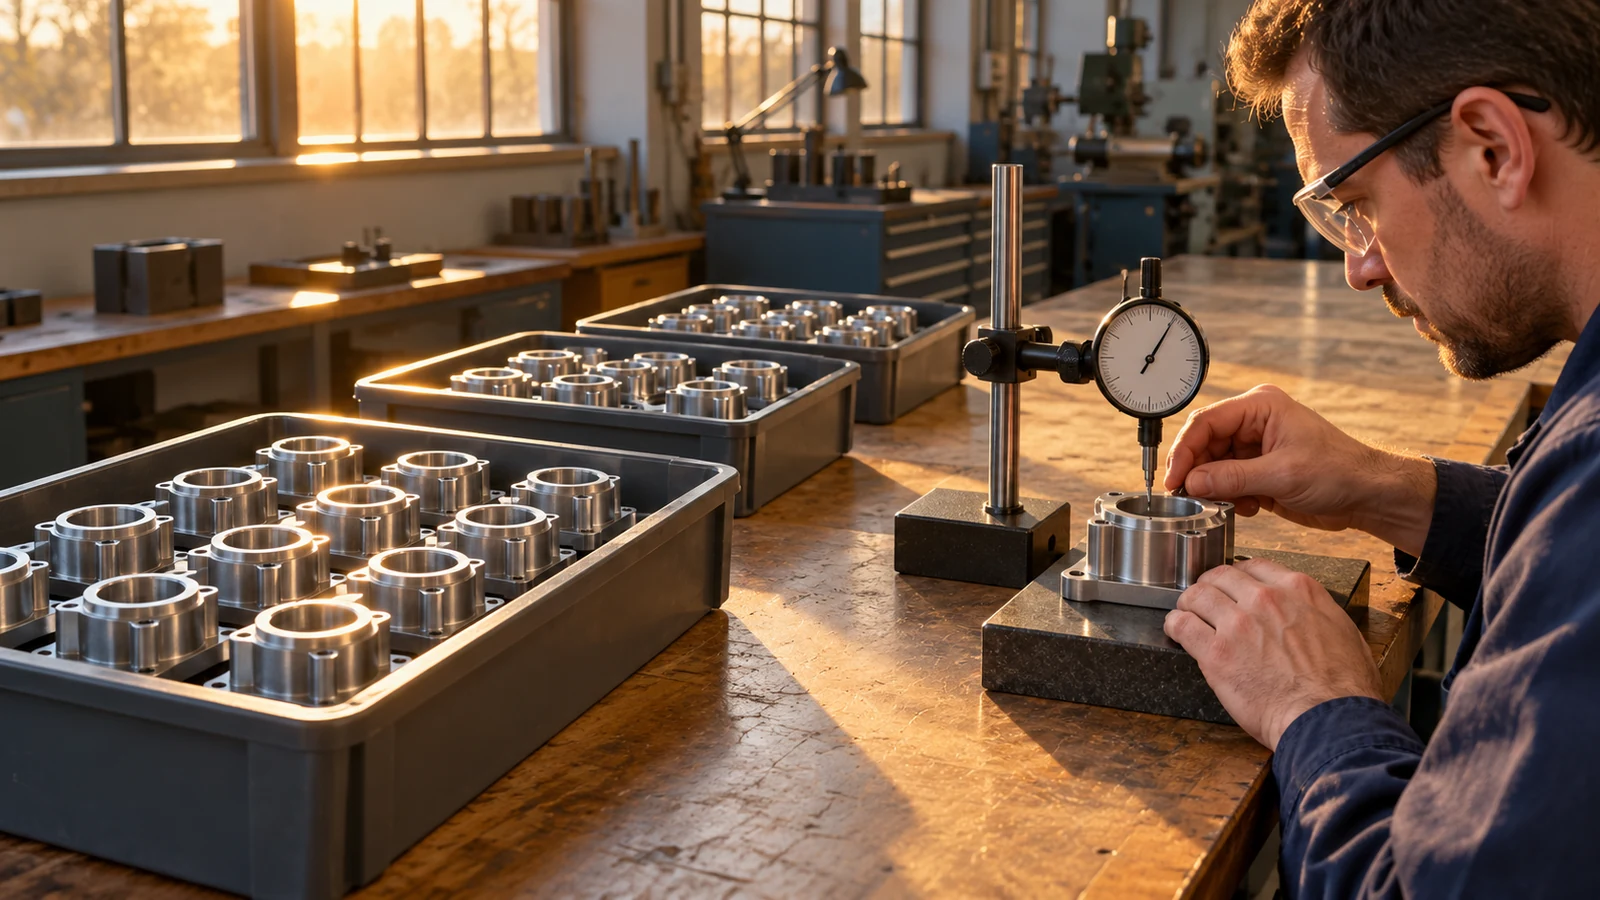
Receiving inspection need not mean measuring every feature on every unit. The organization should decide what verification is appropriate for the part, the supplier’s performance, the process and the consequence of a defect. Evidence may include supplier records, identity checks, selective measurement, functional tests or another justified method.
A certificate of material identity answers a different question from an inspection report. It may support the purchased grade but not prove that a threaded interface fits. Conversely, a dimensional pass does not show whether the approved resin or alloy was used. Define the evidence bundle according to what could go wrong with this component.
If a supplier provides CNC-machined parts, ask how reported dimensions connect to drawing datums and which material lot was used.
For molded parts, discuss tool revision, material identity and any cavity or process conditions relevant to the product. The purchase controls should follow the real process, not an abstract quality template.
Monitor the Supplier After the First Good Lot
Review meaningful performance signals. Repeated borderline dimensions, late change notices, incomplete records, unexplained material substitutions and a rising number of rework requests may matter more than an overall on-time-delivery percentage. The same metric can conceal very different problems if the numerator or review period changes.
Set a response proportional to the issue. A late certificate may need a documentation correction; an unapproved material change may require lot containment and technical assessment. Do not call every late shipment a CAPA, but do not treat a repeated product nonconformance as an administrative inconvenience.
The purchasing organization should revisit supplier status when the device, process or supply route changes. A supplier approved to machine an aluminum prototype is not necessarily evaluated for a later molded production housing. A new subcontracted surface treatment may require its own review even if the original supplier name on the invoice is unchanged.
Show Where Responsibility Changes Hands

One useful exercise is to follow a purchased component through five records: approved design, purchase order, supplier traveler, receiving decision and finished-device build record. If a material or revision changes between them without an identified authorization, the purchasing process has a gap. This exercise is more informative than asking whether a procedure exists in a binder.
Define who can authorize exceptions and how the result is recorded. Procurement may negotiate price and schedule but should not approve a dimensional deviation by itself. Engineering may judge fit yet still need quality or regulatory assessment for a device-level effect. A supplier needs a named contact and a hold rule when approval is pending.
The FDA’s QMSR page confirms the U.S. framework that incorporates ISO 13485:2016 by reference for applicable finished-device manufacturers. It does not make every component purchase automatically compliant. The implemented controls and records must fit the organization’s role and product.
Questions to Put in the Next RFQ

When asking Jucheng to evaluate a component, send controlled 2D and 3D drawings, exact material and finish requirements, quantities, critical features, and the expected inspection or traceability package. Ask what assumptions the manufacturing route depends on and what changes would trigger a new review. A quote based on complete inputs is more useful than a low price attached to an undefined evidence burden.
Purchasing controls create a chain: qualify the source, define the order, verify the output, watch performance and reassess changes. Break any one link and the organization may have an approved supplier without an approved component route.
Is an approved-vendor list sufficient?
No. It records a selection decision, not the requirements of every later order or the supplier’s current performance. The purchasing process needs a way to keep that decision aligned with the component and route being bought.
Must incoming inspection repeat the supplier’s entire inspection?
Not necessarily. The buyer should choose a justified verification method based on the component, supplier controls, contractual evidence and consequences of nonconformance. A reduced incoming check is not the same as having no verification plan.

