

An endoscope distal tip has little room for error. A camera or sensor opening, illumination features, irrigation and suction ports, a working channel, and the distal face all compete for a compact envelope. Each feature may be manufacturable on its own; the difficulty is preserving their relative position while leaving enough material between openings, maintaining a usable surface, and enabling later assembly and inspection.
That makes medical endoscope distal tip machining a component-integration problem as much as a machining problem. The best process discussion begins with the intended function of each opening, the datum scheme, the material and finish requirements, and the verification plan. This article focuses on how those details affect manufacturability and how a design team can communicate them without making unsupported assumptions about the device’s clinical use or regulatory status.
Contents
- Translate the distal tip layout into functional zones
- Make the datum scheme match assembly
- Check wall sections and tool access together
- Choose a route for prototypes and production
- Separate surface finish from cleaning validation
- Plan inspection around inaccessible features
- Prepare a drawing package that supports quoting
- Frequently asked questions
Translate the distal tip layout into functional zones
Start by listing what each feature must do. The imaging aperture must align with the optical or sensor stack. Illumination openings must match the selected light-guide or emitter arrangement. Irrigation and suction paths need defined connections and separation. A working channel must remain open through the intended route. The distal face may also include a lens seat, protective window, bonded interface, or other application-specific feature. These functions are not interchangeable, so the drawing should identify the controlled dimensions and relationships that affect assembly.

Overlay the features on a section view and identify the minimum wall left between adjacent ports, the depth of each bore, the direction of tool entry, and any intersecting channels. The layout review should include the downstream components: lens or window, illumination element, seals, tube connections, and any polymer features that meet the metal tip. This prevents a common design gap in which every hole meets its own diameter callout but the components cannot be assembled in the available space.
Do not use generic dimensions copied from another endoscope. The device architecture, intended use, selected optics, and customer requirements determine the geometry. Similarly, do not infer a validated cleaning or sterilization method from the component name. Those requirements belong to the device specification and validation process. The machining drawing should communicate the features the supplier can manufacture and inspect, while product-level validation remains with the responsible organization.
Make the datum scheme match assembly
Datums should reflect how the tip is located and joined in the final assembly. A primary face or axis may establish the tip orientation; a channel centerline may control the working path; and a clocking feature may orient ports relative to the camera or illumination system. If the component will be bonded, welded, threaded, or joined by another method, the locating surfaces for that operation deserve deliberate definition.
Dimensioning every opening from unrelated edges can create a stack-up that is difficult to interpret. A coherent datum reference frame lets manufacturing establish the part and lets inspection evaluate the same relationships. Where several ports must align with a mating subassembly, position tolerances or profile controls may be clearer than a collection of chained dimensions. The design authority should define the tolerances from functional needs rather than relying on a supplier to select them after the geometry is released.
Consider the order in which references are created. If a narrow body is clamped on a surface that will later be removed, the datum may not survive the route. If a small tip is difficult to hold, the fixture may need to locate from stable external features or a sacrificial carrier. For an early design, a prototype review can identify these setup issues before the tolerance scheme is frozen. The site’s prototyping service can be part of that development conversation when the team needs physical parts to assess fit and assembly sequence.
Check wall sections and tool access together
Miniaturization creates coupled constraints. Moving two ports closer may leave a thin wall; increasing a bore may reduce material around a neighboring seat; deepening a channel may make the entry harder to deburr; and changing the tip length may affect fixture support. Review the complete feature set in section, not just the plan view. Where a wall is functionally important, identify its minimum acceptable condition and how it will be verified after machining.
Tool access should be checked for both cutting and cleanup. A drill can reach a passage and still leave an internal edge that cannot be inspected or safely deburred. The planned cutting tool, holder clearance, approach angle, and chip evacuation path all matter. For intersecting features, decide where burrs are expected and whether the design can provide a controlled edge break or an accessible cleanup route. Small components may need magnification or a purpose-built inspection fixture, but the acceptance method should be agreed rather than assumed.
Material selection influences this review. Stainless steel may be chosen for particular mechanical, corrosion, or device-interface requirements; a polymer may form part of an adjacent component; and other alloys may be specified for a different design. Grade, condition, and surface requirements must come from the approved documentation. The site’s stainless steel machining information is a useful starting point for a material discussion, not a substitute for the released specification. If an adjacent polymer interface is part of the design, the chosen polymer and its machining or molding route should be reviewed separately.
Choose a route for prototypes and production
A one-off prototype and a repeat production component can share the same design intent but not necessarily the same fixture, operation sequence, or inspection economics. A prototype may prioritize rapid learning about port layout, assembly access, and optical alignment. A production route may need stable workholding, controlled setup transfer, documented inspection, and repeatable cleaning and packaging. The quantity, geometry, material form, and release status determine where the route should converge.
| Design question | Prototype review | Repeat-build planning |
|---|---|---|
| Does the layout assemble? | Confirm access, fit, and interface stack with representative parts | Maintain controlled datums and revision traceability |
| Can internal edges be controlled? | Identify burr locations and practical cleanup access | Define the repeatable deburr and verification method |
| Are critical relationships measurable? | Use the build to refine the inspection approach | Agree gauges, sampling, reports, and reaction steps |
| Is the specified material available? | Document any approved prototype-only substitution | Control grade, condition, source, and lot records as required |
For a machined tip, roughing and finishing may be separated to protect small seats and reference surfaces. For a design with formed or molded elements, the assembly route may determine when the metal feature is completed. Avoid calling any sample “production representative” unless the materials, process, and test scope justify that description. Record what the prototype did and did not evaluate.
Separate surface finish from cleaning validation
Surface finish is a drawing and interface requirement; cleanliness is a process and verification requirement. They may interact, but one does not prove the other. A specified roughness may apply to a lens seat, sealing region, or mating face, while other surfaces may have different functional needs. Marking the whole component with one finish can add cost or obscure which surfaces actually matter.
For every controlled surface, state the finish parameter and the measurement location or method when necessary. Protect optical seats and bond surfaces during handling. If a coating or passivation step is required, identify affected areas, masking boundaries, dimensional allowances, and post-process inspection. The site describes surface finishing options that can inform an early conversation, but compatibility with the device design, cleaning agents, and validation protocol must be established by the project owner.
Cleaning instructions should identify the residue or particle concern, the process endpoint, and the evidence expected. A supplier can describe its available cleaning and inspection workflow, but cannot assume the customer’s validated cleanliness threshold. Packaging matters too: a clean component can be recontaminated by contact, loose packaging, or mixed-lot handling. Specify protection, labeling, and traceability through delivery.
Plan inspection around inaccessible features
Inspection planning should separate directly measurable dimensions from characteristics that need a derived method. External dimensions, accessible faces, and visible ports may be checked with conventional metrology. Internal channel continuity, hidden intersections, and very small wall sections may require a defined gauge, imaging method, fixture, or functional test. Each method has limits; an optical image, for example, may show an entrance edge but not prove the condition of an entire internal passage.
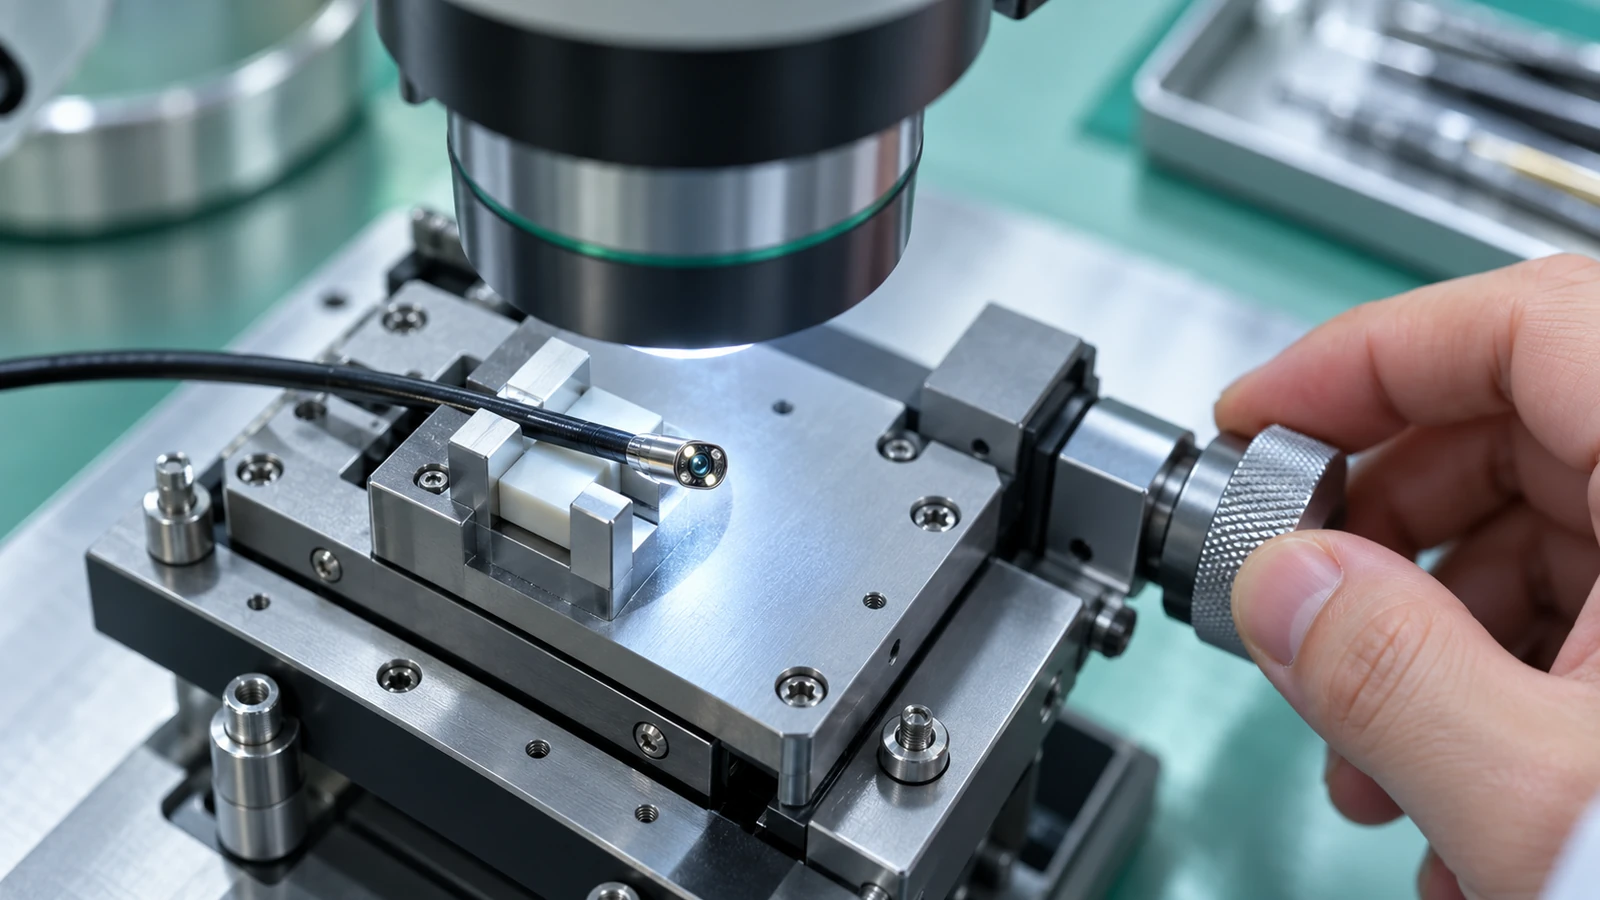
For critical interface relationships, agree how the part is located during measurement and which datum references are used. A report should identify the drawing revision, feature number, measurement result, and equipment or method where required. If a functional assembly test is used as evidence, define the fixture and pass criteria. A component should not be judged against an unwritten tolerance or test that was never part of the released requirements.
For low-volume development, inspection can also be used to learn where the drawing is ambiguous. If the team repeatedly debates which edge defines a port position or how a channel is checked, update the drawing before the next build. This makes the specification more useful for both manufacturing and incoming quality review.
Prepare a drawing package that supports quoting
Provide a fully dimensioned drawing or controlled model, revision, material and condition, finish notes, quantity, critical characteristics, inspection expectations, cleaning and packaging requirements, and the intended assembly interfaces. Include section views through intersecting channels and identify features that cannot be inferred from a rendered model. Clearly label preliminary geometry and unresolved decisions.
Ask the supplier to identify assumptions about fixture access, tool reach, burr removal, inspection method, outside processing, and lead time. A useful manufacturability review should point to specific features and tradeoffs, not simply say that the part is manufacturable. When a design revision changes a port location, wall section, or datum, evaluate its effect on fixtures and prior inspection programs before approving the next build.
For broader context, the site’s medical device manufacturing processes overview connects component fabrication to the larger production system. The endoscope tip still needs its own clear drawing intent, process route, and verification plan; a general industry page is not a substitute for part-specific requirements.
Frequently asked questions
Which features usually drive endoscope tip machining complexity?
Closely spaced ports, intersecting passages, small remaining walls, optical or sealing seats, and datum relationships to the assembly are common drivers. The actual priorities depend on the device design and drawing.
Can machining alone establish device cleanliness or clinical suitability?
No. Machining can meet defined geometry and process requirements, but cleanliness validation, sterilization validation, and clinical suitability are product-level responsibilities governed by the applicable device documentation and qualified processes.
Should every port have the same tolerance?
Not necessarily. Tolerances should follow function, assembly relationships, and the ability to measure the feature. The design authority should distinguish critical interfaces from noncritical geometry.