

A satellite antenna mount is a mechanical interface that supports an antenna and locates it relative to the spacecraft structure. Manufacturing planning should preserve the defined mounting plane, bolt pattern, orientation references, stiffness features, and access needed for assembly and inspection. A mount that fits its bracket but shifts the antenna reference frame can still miss the system’s alignment intent.
“Satellite antenna mount” can describe anything from a compact instrument bracket to a large support structure. This article focuses on the part-level decisions for a custom mount or prototype and does not prescribe spacecraft loads, pointing performance, or mission qualification.
Contents
- Define the antenna and spacecraft reference frames
- Geometry must preserve access and alignment
- Choose a route around size, stiffness, and interfaces
- Account for the environment without inventing limits
- Separate dimensional checks from system validation
- Build an RFQ around the interface package
- Frequently asked questions
Define the antenna and spacecraft reference frames
The mount links at least two reference systems: the antenna’s mounting definition and the spacecraft structure’s interface. These may use different datums or coordinate conventions. The released drawing should show how the mounting plane, bolt pattern, orientation features, and any local datum targets relate to the spacecraft reference.
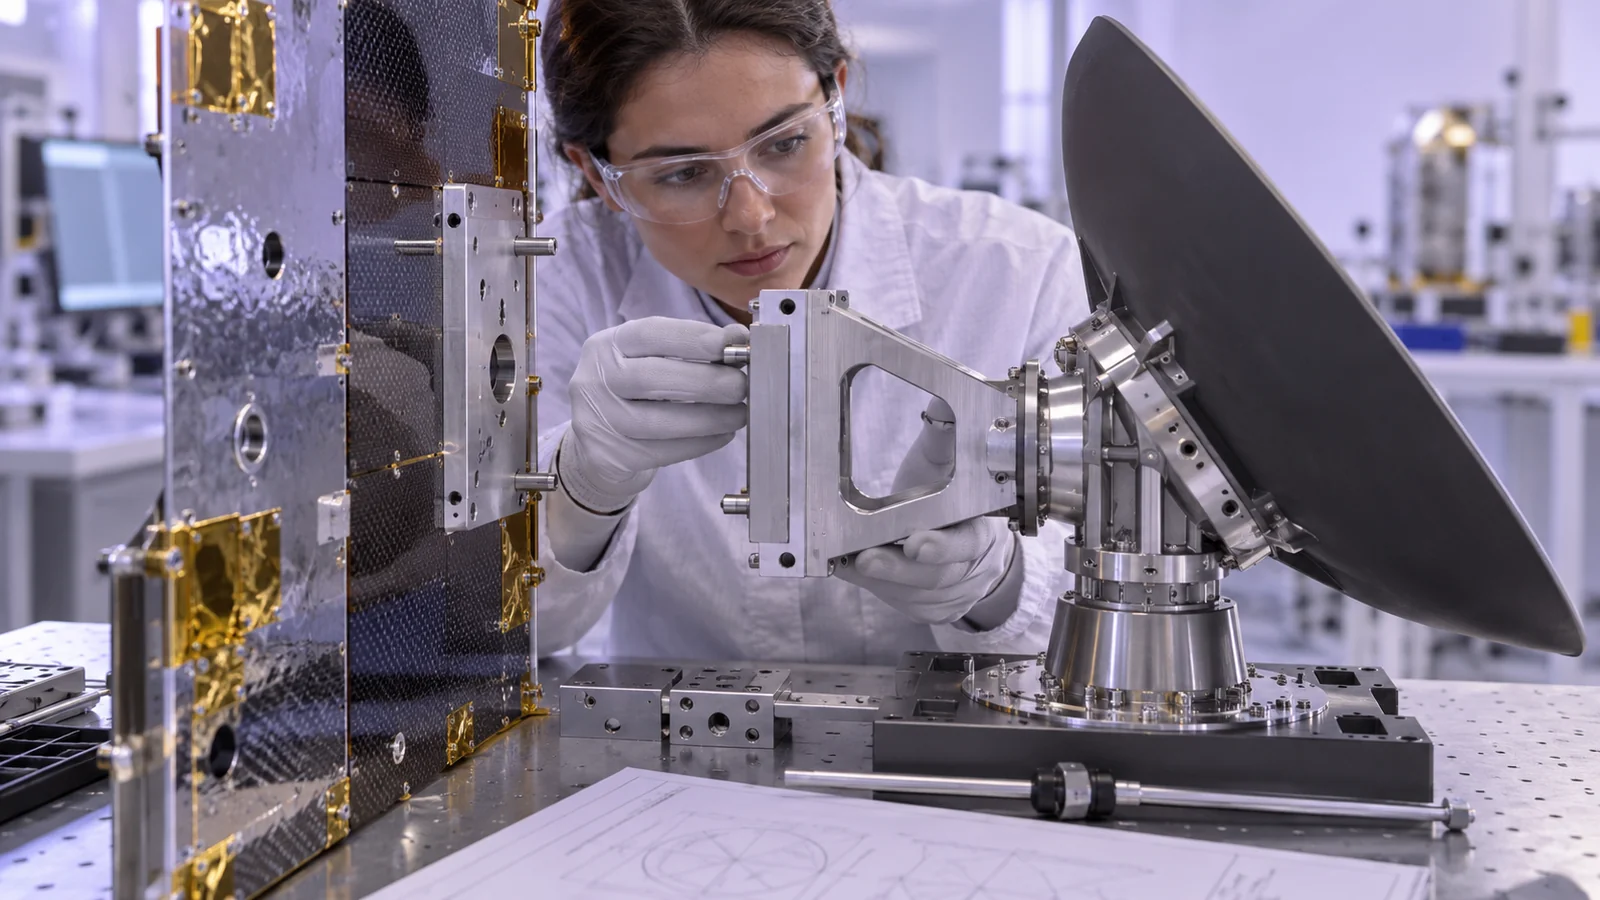
Before manufacturing begins, confirm which faces locate the mount, which holes establish orientation, and how the antenna’s line-of-sight reference is represented in the mechanical definition. The supplier should not calculate pointing performance from incomplete assembly data. The manufacturer can produce features to a defined interface and report measured results against that definition.
Use the Aviation and Aerospace industry page as the parent context, then keep the detailed mount interface in the controlled drawing package.
Geometry must preserve access and alignment
A compact mount can include thin walls, ribs, pockets, cable clearances, fasteners, and adjustment features. Each has a different function. A lightweight pocket may reduce mass but leave a flexible wall; a recessed fastener may improve packaging but make tool access difficult. The design should identify where stiffness, alignment, and assembly access control the geometry.
Check the sequence in which hardware will be installed. A tool path for machining may be clear while the final fastener path is blocked by a cable, bracket, or enclosure. Assembly access should be reviewed against the full configuration rather than the bare mount alone.
For a development build, keep tolerance decisions linked to the interface. Adding tighter tolerances everywhere can raise inspection effort without improving the antenna reference relationship. Focus the inspection on the mounting plane, locating features, and any controlled orientation characteristic.
Choose a route around size, stiffness, and interfaces
A small mount with complex pockets may be suited to CNC machining from a specified blank. A larger support may use a different structure or multiple parts. Additive manufacturing can be evaluated for development geometry when material, post-processing, and verification requirements are defined. A sheet-metal bracket may be suitable for a different architecture. The route must follow the approved design and mission requirements.
| Design condition | Manufacturing review | Inspection focus |
|---|---|---|
| Several angled interfaces | Tool access, setup count, and datum transfer | Relative position of mounting faces |
| Thin webs or pockets | Support, material removal sequence, and free-state movement | Profile and stiffness-related geometry required by drawing |
| Large envelope | Blank sourcing, machine travel, handling, and fixture support | Full-length or full-span reference relationships |
| Prototype iteration | Change control, material representativeness, and cost per revision | Which measurements answer the development question |
Where several faces or orientations are involved, review the five-axis machining process as one option for access planning. For an early geometry model, the aerospace 3D printing service may support a prototype when the intended evaluation permits that material and route.
Account for the environment without inventing limits
Space hardware may face launch loads, vibration, thermal cycling, vacuum, and other environment-specific conditions. The actual environment and acceptance limits belong to the spacecraft program. A part supplier needs the controlled requirements that apply to the mount and should not guess a load, temperature range, or qualification test from the application name.
Environmental requirements can affect material, fasteners, coatings, surface preparation, and contamination controls. They can also change how the component is inspected or documented. If the order requires a particular test or material record, identify it before quote acceptance and clarify whether it is included in the supplier scope.
A prototype used for packaging may not represent a flight hardware material or process. Label its status and preserve the difference in the traveler and delivery records.
Separate dimensional checks from system validation
Dimensional inspection can verify specified mount geometry, but it does not prove antenna performance or spacecraft pointing accuracy. Those outcomes depend on the broader system, installation, calibration, and program-level verification. Keep supplier inspection reports limited to the characteristics actually measured.
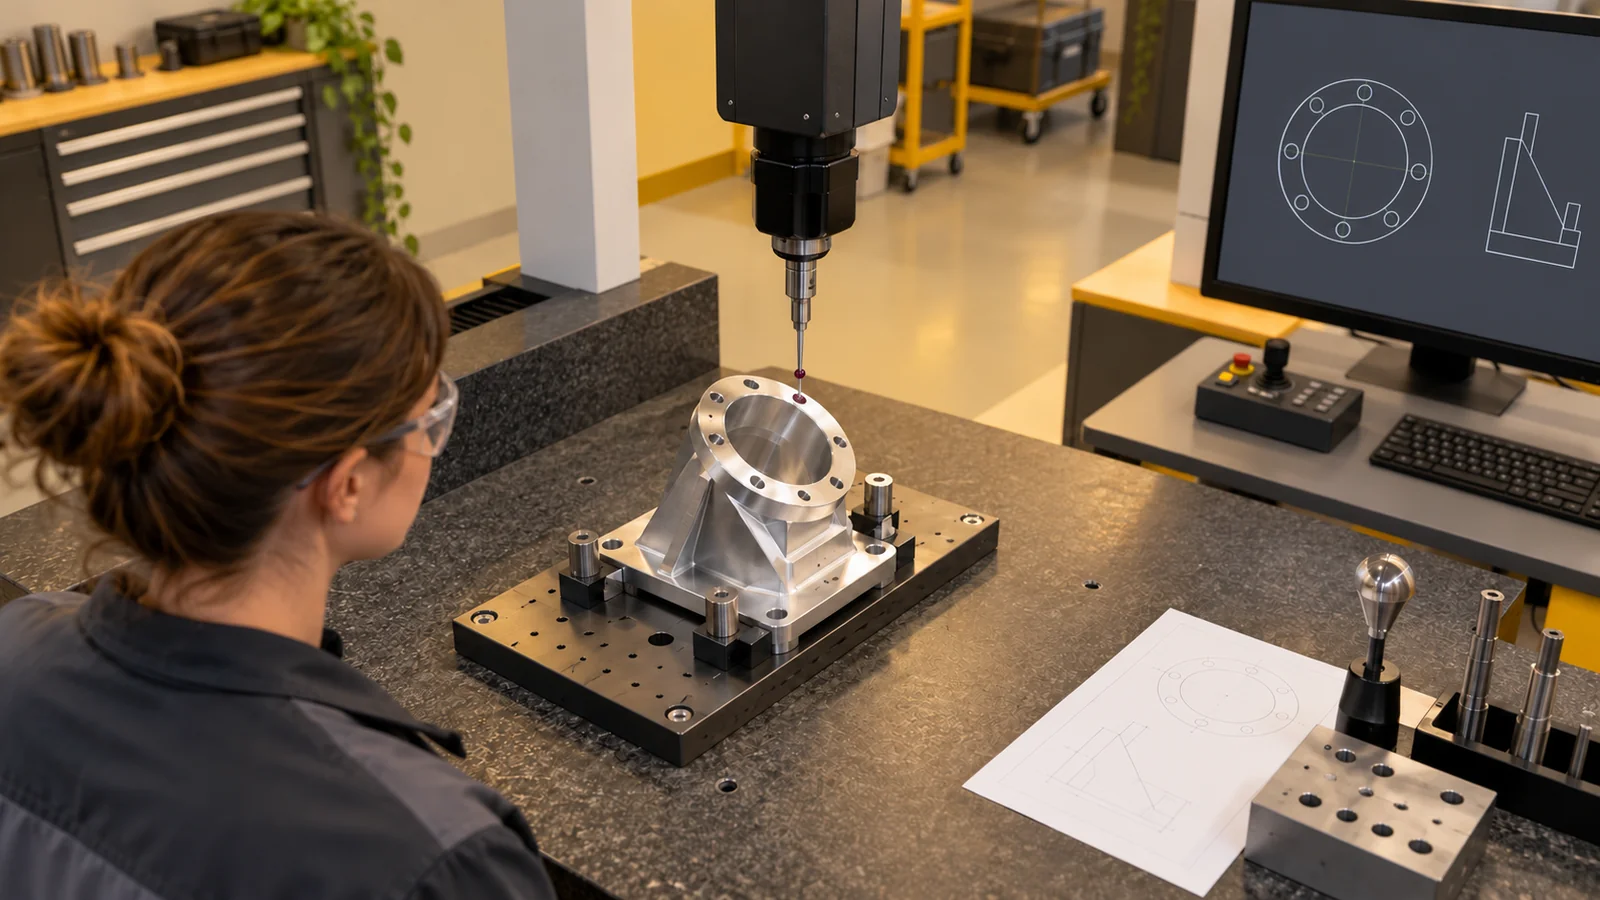
For the mount itself, define the datum alignment, measurement condition, controlled features, and result format. If the antenna is installed during a fit check, specify whether the check evaluates only mechanical clearance or a larger system requirement. That distinction prevents a simple fit observation from being interpreted as mission-level validation.
Where a feature becomes inaccessible after assembly, choose whether to inspect it before installation, use an in-process record, or define an approved assembly-level check. Make that choice before the part is built.
Build an RFQ around the interface package
Include the part drawing and model, interface control information, material and condition, quantity, finish, critical features, inspection expectations, environmental requirements, and required documentation. Identify the intended purpose of a prototype and state which characteristics are frozen versus likely to change.
Ask the supplier to identify assumptions about fixture orientation, coordinate transfer, inspection access, and delivery packaging. If the mount has multiple revisions or left/right variants, separate them clearly to prevent a file or part-number mix-up.
Review quote scope for manufacturing operations, post-processing, inspection, and any buyer-provided hardware. A transparent scope is easier to compare than a low unit price that omits required records or assembly checks.
Frequently asked questions
Does a satellite antenna mount determine pointing accuracy by itself?
No. It provides a mechanical interface. Pointing performance depends on the antenna, installation, spacecraft reference system, calibration, and program-level validation.
Can a 3D-printed mount be used as flight hardware?
Not by default. The approved design, material, process, post-processing, inspection, and qualification requirements must support that intended use.
Which dimensions should be prioritized in inspection?
Use the controlled drawing to identify the mounting plane, locating features, bolt pattern, and orientation relationships that define the interface. The required method and tolerance come from the program.
What should a prototype mount be used to prove?
State whether it is for envelope, access, assembly sequence, or another limited development question. A prototype does not automatically demonstrate environmental or mission performance.
A satellite antenna mount is best sourced as a defined interface, not as an isolated bracket. When the coordinate relationship, inspection scope, and prototype boundary are explicit, the supplier can plan manufacturing around the mechanical requirements without implying that dimensional acceptance alone validates the spacecraft system.

