

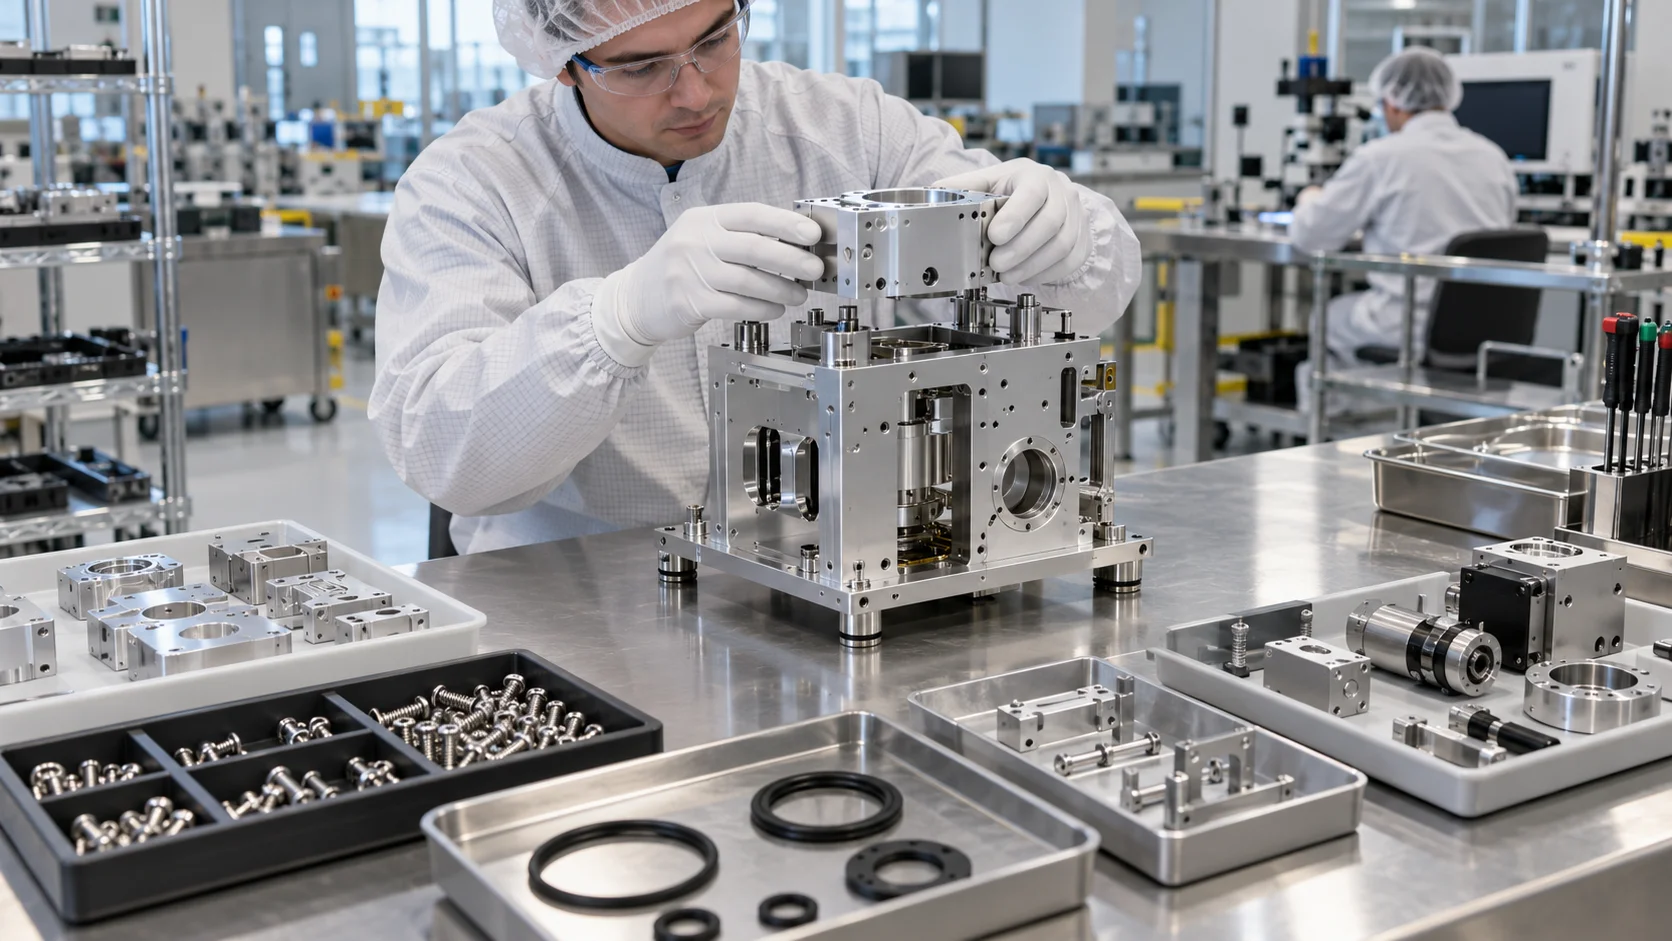
A semiconductor equipment program can fail at the handoff between individual parts and the installed module. The components may be within tolerance, yet assembly can slow down because revisions, fasteners, interfaces, packaging, or supplier responsibilities are unclear. A reliable supply plan treats assembly as an engineering process with its own inputs and checks.
Decide what the supplier owns
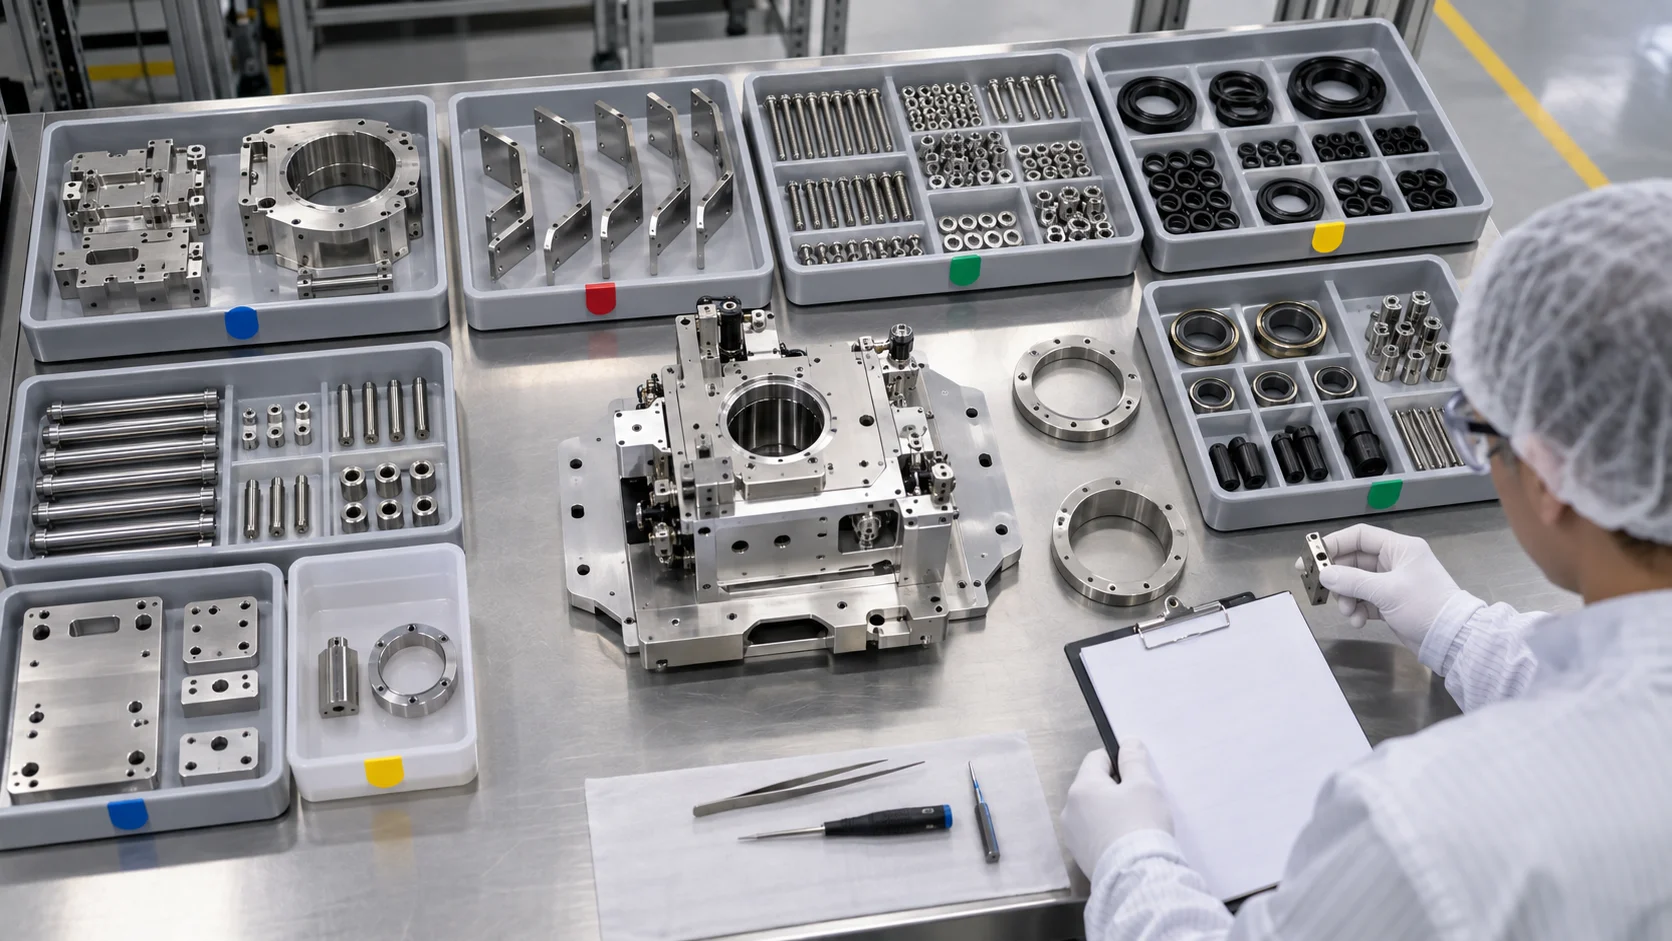
Clarify whether the supplier is making parts only, preparing kits, performing mechanical assembly, or delivering a tested subassembly. Each scope has different responsibilities for hardware, torque, alignment, cleaning, labeling, and inspection.
A partner that covers semiconductor equipment parts manufacturing can often connect component production with assembly, but the purchase order should still state the exact deliverable.
Build a BOM people can execute
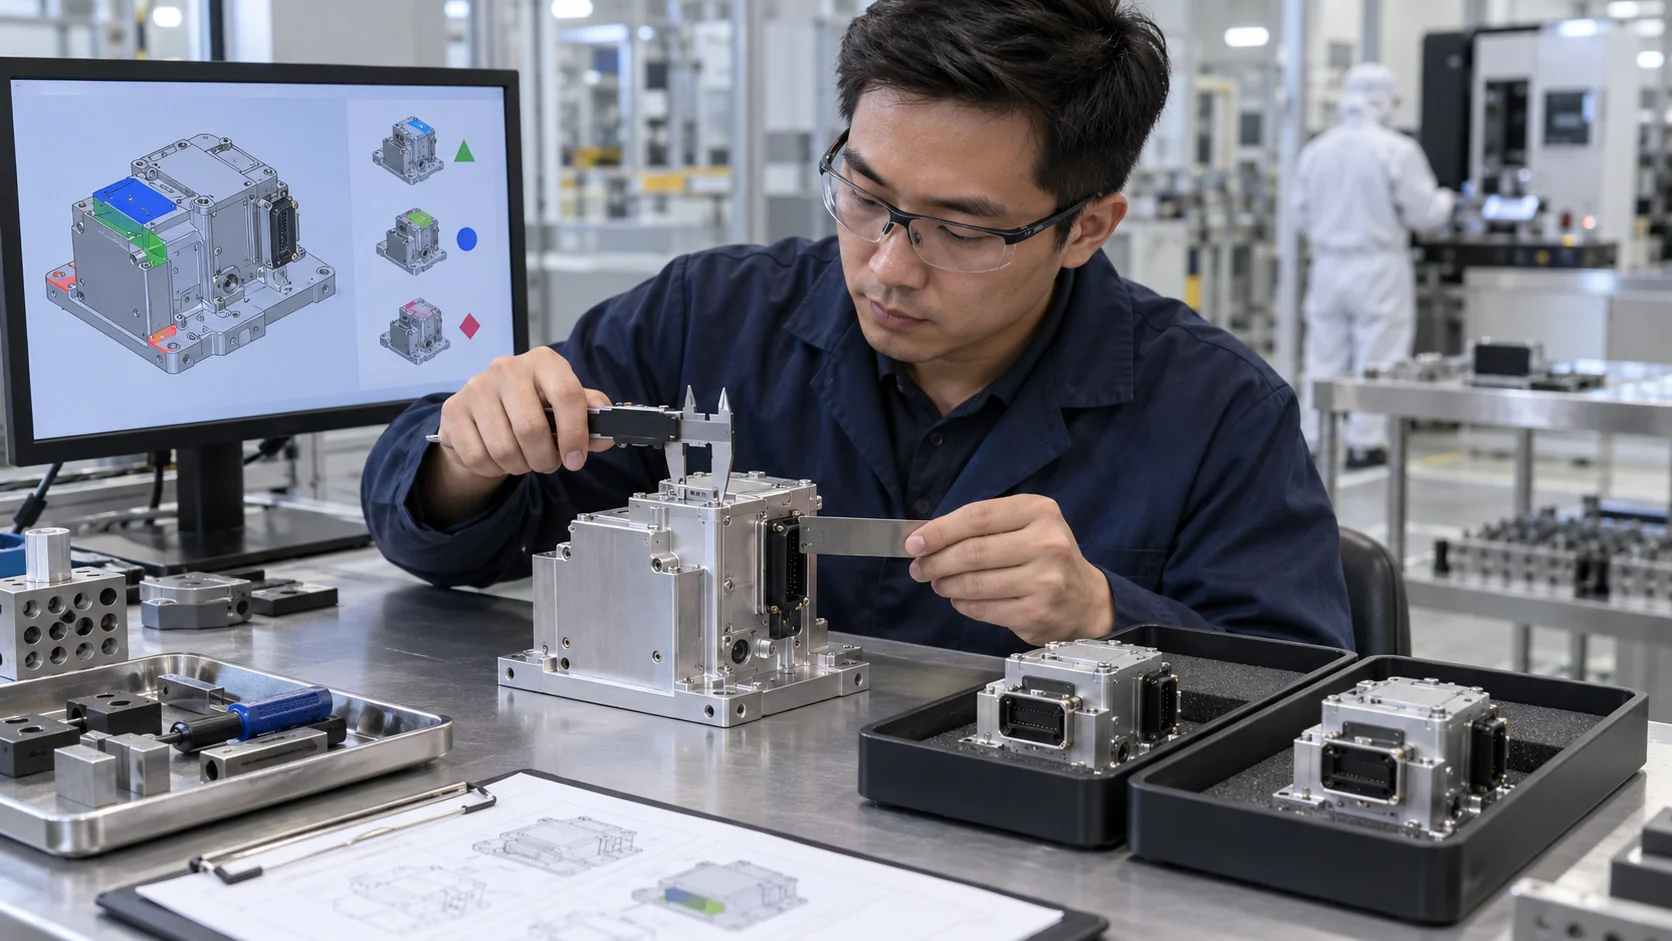
The bill of materials should identify part number, revision, quantity, material, finish, approved substitute, and assembly position. Add fasteners, seals, shims, purchased items, and consumables when they affect the finished module. A partial BOM forces the assembler to resolve engineering questions on the shop floor.
| BOM field | Why it matters |
|---|---|
| Revision | Prevents mixed versions in one build |
| Quantity per assembly | Reveals shortages before kitting |
| Material and finish | Controls function and handling |
| Inspection status | Shows whether a part is ready to install |
Protect interfaces and revisions
Assembly problems often appear at interfaces: a hole pattern, locating shoulder, cable opening, seal groove, or connector clearance. Identify these features on the drawing and verify them before the full module is built.
For sheet metal modules, coordinate fabrication with the existing assembly service so access and fastening are reviewed together. Any engineering change should state which parts, instructions, and inspection records are affected.
Inspect at the handoffs
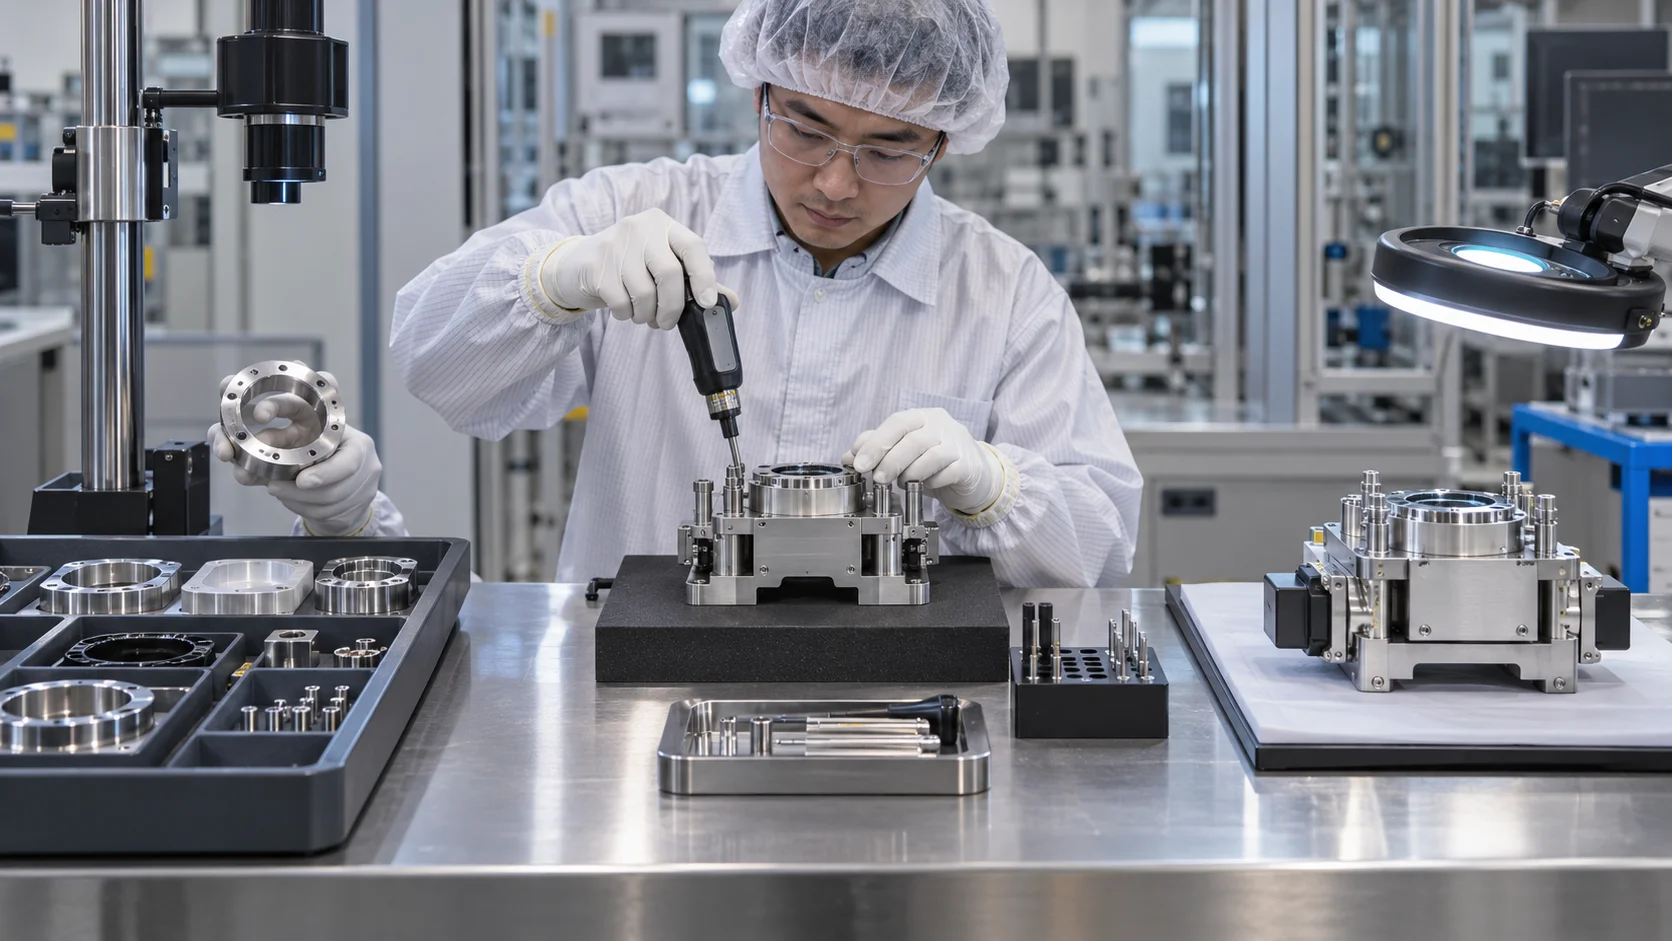
- Incoming check: confirm part number, revision, quantity, and visible condition.
- Pre-assembly check: verify critical dimensions, threads, surfaces, and hardware.
- In-process check: confirm alignment, torque, clearance, and orientation.
- Final check: record appearance, function, labels, and packing condition.
Staged checks make it easier to locate the source of a problem. They also create evidence that a module was assembled from the approved parts rather than from mixed revisions.
Plan continuity before the first shipment
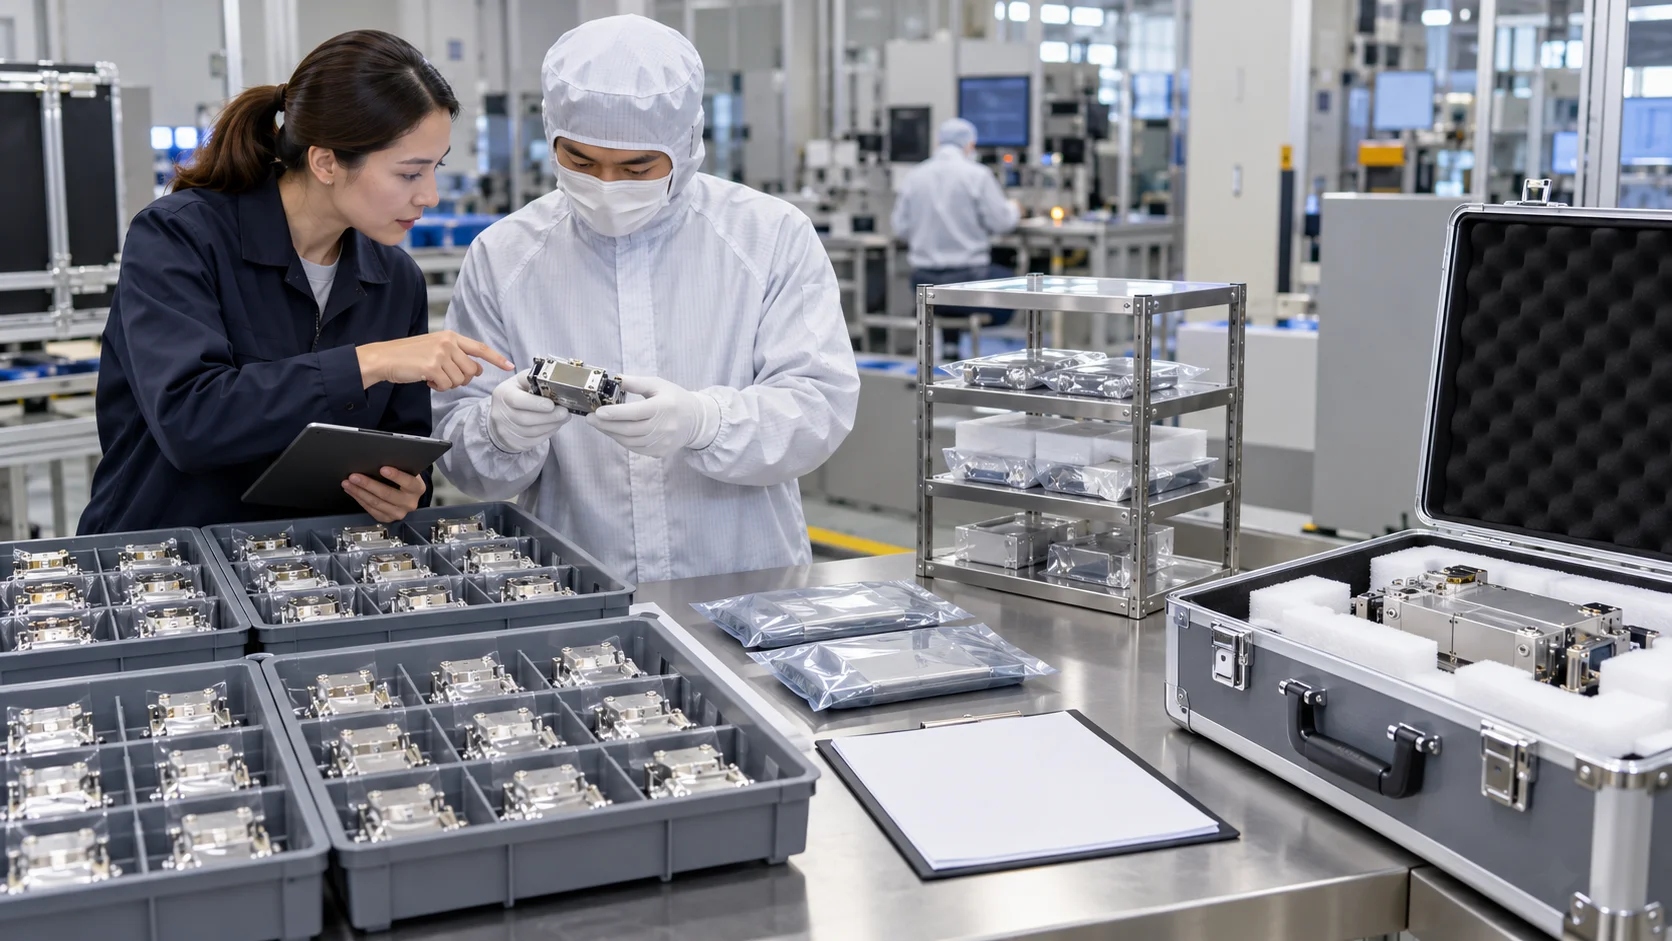
A supply plan should account for prototype builds, pilot quantities, repeat orders, spares, and engineering changes. Keep the drawing package, inspection records, supplier questions, and packing method available for the next order. This is especially important for low-volume equipment where demand may be irregular.
For precision components, a documented CNC milling route can support repeat production when the datum and inspection strategy are retained.
Assembly handoff checklist
- Freeze the BOM and revision before assembly begins.
- Confirm interface, fastener, cleanliness, and inspection requirements.
- Define what is checked at incoming, in-process, and final handoff.
Assembly and Supply Questions
What is included in semiconductor equipment assembly?
It may include kitting, mechanical joining, alignment, fastening, cleaning, labeling, inspection, and delivery of a defined subassembly. The exact scope should be written into the project requirements.
Why do correct parts still create assembly delays?
Common causes include mixed revisions, incomplete BOM data, unclear interfaces, missing hardware, poor access, or inspection performed too late.
The Assembly Handoff
Assembly reliability comes from connecting part production, documentation, interfaces, inspection, and supply continuity. When these elements are planned together, semiconductor equipment teams spend less time resolving preventable handoff problems.

